
 Register

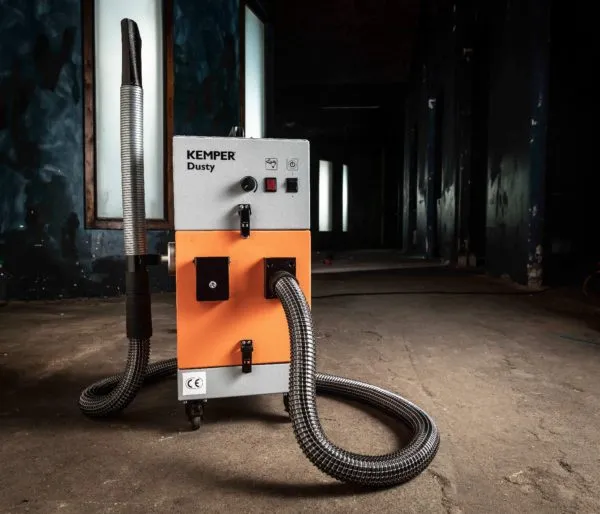
Dusty High Vacuum Filter Unit
- Kemper’s Dusty High vacuum welding smoke extraction unit is equipped with two suction nozzles for sporadic use. For example, the Dusty can be used in repair work, or for mobile use with low to medium amounts of dust. The manually cleanable KemTex® ePTFE filter cartridge makes the unit particularly economical.
Applications
- Low to medium levels of smoke and dust
- Torch extraction
- Repair work
- Alternating workplaces
Benefits
- Best health protection for employees by use of KemTex® ePTFE filter cartridges with surface filtration
- For mobile use due to light weight
- Optimal adjustment to the welding process with stepless speed control
Technical Data
- Filter Stages: 1
- Filter Method: Cleanable Filter
- Filter Surface: 1.35 m²
- Type of Filter: Filter Cassette
- Filter Material: ePTFE-membrane
- Filter Efficiency: > 99.9%
- Dust Classification: M
- Input Voltage: 1x220 V
- Frequency: 50 Hz
- Motor Power: 1.6 kW
- Extraction Capacity: 340 m³/h
- Noise Level: 74 dB(A)
- Dimension: 300 x 300 x 690 mm
- Weight: 21 kg.


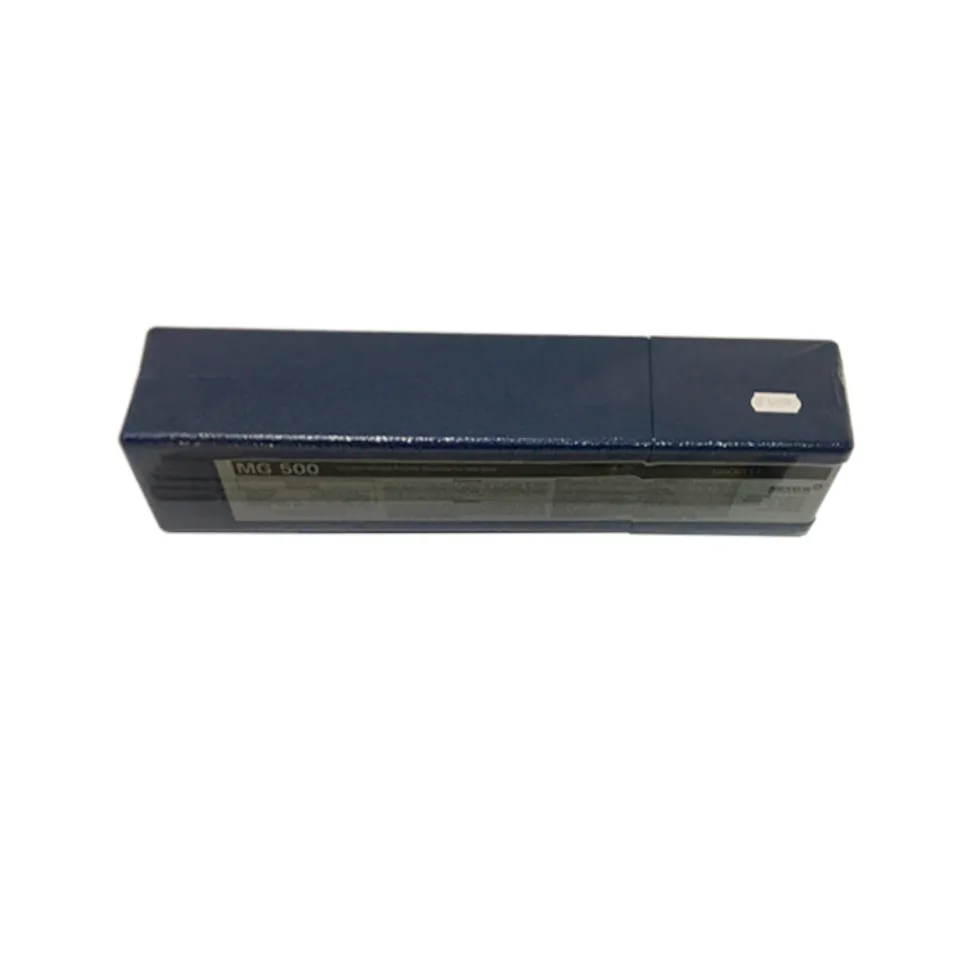
MG 500 – EASIEST-TO-USE, ALL POSITION ELECTRODE FOR MILD STEEL
- Diameter 4.0 x 350 mm
- Weight 5.0 kg
General Characteristics
This electrode has been designed to operate on almost any AC or DC welding machine even when the open circuit voltage is very low. The special coating protects the weld deposit from adverse conditions normally encountered in maintenance repair welding. Low amperage requirement controls distortion when welding thin sheet metal; spatter is kept to a minimum. Ideal for field repair work and out-of-position welding.
Application
Fabrication of thin, medium, heavy and dissimilar gauge mild steels. Sheets, plates, angle iron, beams, pipes and machine parts can be welded in all positions. Also used for filling holes and build-up of over-machined and worn surfaces. Commonly used on applications requiring short, intermittent and spot welds because of the outstanding restarting characteristics.
Technical Data
- Tensile Strength: 80,000 psi
- Yield Strength: 68,000 psi
- Elongation: 24%
- Current: AC or DC Either Polarity
Procedures
Remove as much foreign material as practical from the weld area. DC reverse polarity (electrode +) produces deep penetration; DC straight polarity (electrode -) will have limited penetration and a flatter bead. AC prevents arc blow. A medium arc length should be maintained with either stringer or weave beads. Slag is easily removed with a light chipping hammer.