
 Register

Inverter Plasma Cutting Machine
- The single-phase power source with inverter technology for metal plasma cutting, PLASMA 36 COMPRESSOR PFC INVERTER, includes a built-in air compressor (maintenance free self-lubricating piston) assuring the operator total work independence and ease of use, since it does not require air adjustment.
Functions
- Pilot Arc to cut painted or coated metals.
- Post-gas function.
- Electronic regulation of cutting current.
- Microprocessor-controlled cutting parameters and functions.
- Thermostatic protection.
- Electronic regulation of cutting current.
Technical Data
- Input Voltage: 1x220 V
- Frequency: 50/60 Hz
- Cutting Current: 20 A
- Duty Cycle: 20 A / 30% , 18 A / 60% , 15 A / 100 %
- Cutting Thickness on Steel: 12 mm
- Max. Separation Cut: 16 mm
- Protection Class: IP23
- Dimension: 210 x 350 x 460 mm
- Weight: 16.0 kg.


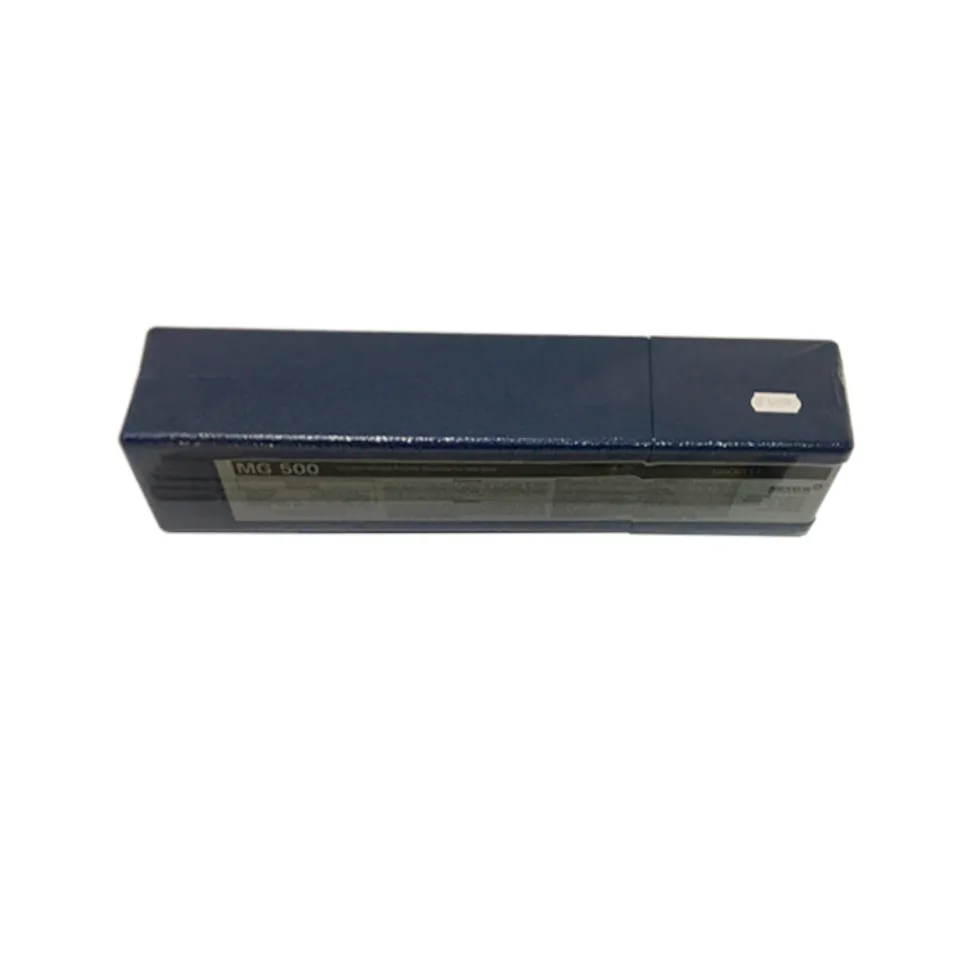
MG 500 – EASIEST-TO-USE, ALL POSITION ELECTRODE FOR MILD STEEL
- Diameter 4.0 x 350 mm
- Weight 5.0 kg
General Characteristics
This electrode has been designed to operate on almost any AC or DC welding machine even when the open circuit voltage is very low. The special coating protects the weld deposit from adverse conditions normally encountered in maintenance repair welding. Low amperage requirement controls distortion when welding thin sheet metal; spatter is kept to a minimum. Ideal for field repair work and out-of-position welding.
Application
Fabrication of thin, medium, heavy and dissimilar gauge mild steels. Sheets, plates, angle iron, beams, pipes and machine parts can be welded in all positions. Also used for filling holes and build-up of over-machined and worn surfaces. Commonly used on applications requiring short, intermittent and spot welds because of the outstanding restarting characteristics.
Technical Data
- Tensile Strength: 80,000 psi
- Yield Strength: 68,000 psi
- Elongation: 24%
- Current: AC or DC Either Polarity
Procedures
Remove as much foreign material as practical from the weld area. DC reverse polarity (electrode +) produces deep penetration; DC straight polarity (electrode -) will have limited penetration and a flatter bead. AC prevents arc blow. A medium arc length should be maintained with either stringer or weave beads. Slag is easily removed with a light chipping hammer.